A foreign material control food manufacturing program prevents credible physical contaminants, detects what prevention cannot eliminate, and controls affected product when a finding occurs. For powdered ingredients, the program must connect raw-material sources, equipment wear, personnel, packaging, inspection devices, and incident records.
Buyers using foreign material control food manufacturing criteria for culinary matcha should ask which contaminants are credible at each process stage and which control can actually intercept them. Microbiological testing answers a different hazard, and one detector cannot compensate for every physical source.
Foreign material control in food manufacturing begins with credible physical-contaminant sources. Prevention, separation, detection, rejection, investigation, and trending have different jobs. Equipment capability must be validated with the actual product and pack.
In short:
Key points:
- Define the exact item, process, evidence and decision in scope.
- Match controls to the credible mechanism instead of copying a generic template.
- Retain ownership, exceptions, change triggers and verification evidence.
What is foreign material control in food manufacturing?
Foreign material control in food manufacturing is a system for preventing, detecting, segregating, and investigating unwanted physical material. The FDA compliance policy identifies traumatic-injury risks and discusses 7–25 mm hard or sharp objects in certain ready-to-eat or minimally prepared foods. Intended use and consumer context govern that policy; 7 mm is not a universal release limit. Keep this system distinct from the broader food-manufacturing sourcing guide and use the supplier audit guide without replacing line controls.
The system begins with a source-specific hazard analysis and ends with documented disposition. It should distinguish naturally occurring material, equipment fragments, personal items, maintenance debris, and packaging fragments because each calls for different prevention and detection.
Control performance depends on product form, contaminant properties, equipment position, packaging, flow, and line speed. A buyer should therefore review the process and its records rather than ask for a universal “metal-detected” statement.
Define responsibility for prevention, device operation, investigation, disposition, and trend review. A control without release authority leaves operators able to find a problem but unable to protect the affected lot.
Specifications should state the control expectation and reporting route without promising impossible absence. The supplier and buyer also need agreement on evidence preservation, complaint notification, and who decides disposition when a physical finding appears after receipt.
Key Takeaway: Foreign material control in food manufacturing is a system for preventing, detecting, segregating and investigating unwanted physical material.
How should a foreign-material source map be built?
Map credible sources at receiving, storage, opening, processing, maintenance, packing, and transport. FDA notes that objects below 7 mm can still matter for special-risk groups and that subsequent processing may change the hazard. The source map must therefore include intended users and downstream preparation rather than relying on one size cutoff.
Walk receiving, opening, conveying, milling, screening, blending, packing, storage, maintenance, and cleaning. At each step, ask what can break, loosen, fall, or arrive with the material. Connect the source to product state and the next point where it can be prevented or intercepted.
Review the source map after new equipment, repairs, packaging changes, supplier changes, or findings. The map should retain closed sources so recurring material can be compared with past investigations.
Key Takeaway: Map credible sources at receiving, storage, opening, processing, maintenance, packing and transport.
Which preventive controls reduce physical contamination?
Use supplier controls, protected storage, tool accountability, preventive maintenance, brittle-material programs, and controlled opening practices according to source. Under 21 CFR 117.80, food manufacturing, packing, and holding must use adequate sanitation principles and appropriate quality-control operations. The provision specifically identifies protection against metal or other extraneous material through sieves, traps, magnets, electronic metal detectors, or other suitable effective means.
Prevention includes supplier specifications, incoming inspection, container-opening rules, tool accountability, preventive maintenance, equipment condition checks, brittle-material control, controlled clothing, and packaging integrity. Choose measures from the mapped source rather than installing equipment first.
This food CGMP provision supports layered controls rather than a universal device. Eliminate a credible source where practical before relying on downstream detection; otherwise recurring fragments create holds, investigations, and possible customer exposure.
Inspect prevention where work occurs. A maintenance procedure may require tool reconciliation, but the completed job record should show which tools and parts entered and left the area before product resumes.
| Source family | Preventive control | Verification evidence |
|---|---|---|
| Incoming material | Supplier requirement and receipt inspection | Lot and inspection record |
| Equipment wear | Condition checks and planned maintenance | Work order and pre-start review |
| People and tools | Controlled items and accountability | Shift or task record |
| Packaging | Line clearance and material inspection | Changeover and reconciliation |
Key Takeaway: Use supplier controls, protected storage, tool accountability, preventive maintenance, brittle-material programs and controlled opening practices according to source.
How should sieves and screens be controlled?
Specify mesh or aperture, material, location, flow condition, inspection, integrity checks, and disposition after damage. In its meat and poultry directive, FSIS describes checking detection equipment with seeded samples of a specified size and maintaining calibrated limits. Matcha suppliers still need validation for their product, equipment, package, and operating conditions.
Specify aperture, construction, location, installation, inspection method, and product flow. Check integrity at defined points and reconcile any missing wire or screen fragment. A clogged or bypassed sieve can change flow without being visibly broken, so operators need criteria for both damage and performance.
If damage is found, define the potentially affected interval from the last acceptable check. Hold material, inspect equipment, investigate fragments, and decide whether re-screening is technically adequate. A later intact check cannot prove earlier product was protected.
Trend screen residue separately from screen integrity. Increased oversize material may reflect incoming conditions or process change, while broken mesh points to equipment failure and a different affected-product assessment.
Key Takeaway: Specify mesh or aperture, material, location, flow condition, inspection, integrity checks and disposition after damage.
What can magnets control?
Magnets can capture susceptible ferrous material when field, configuration, product flow and cleaning are suitable. They do not remove nonferrous metal, glass, stone or plastic. Trend findings by location and morphology to identify equipment wear. Do not report magnetic strength or cleaning frequency without validated site evidence.
Magnets can capture susceptible ferrous material when strength, placement, exposure, cleaning, and product flow are suitable. They do not control every metal, and accumulated material can reduce performance or indicate upstream wear.
Define inspection and cleaning without contaminating product. Trend what is removed by appearance, quantity, location, and timing, while avoiding unsupported composition claims. Repeated findings should trigger upstream equipment review instead of being celebrated as proof the magnet works.
Magnet verification should cover installation and condition as well as any specified strength check. A strong magnet mounted where product has poor contact may deliver less control than the certificate suggests.
Key Takeaway: Magnets can capture susceptible ferrous material when field, configuration, product flow and cleaning are suitable.
When are metal detection and X-ray appropriate?
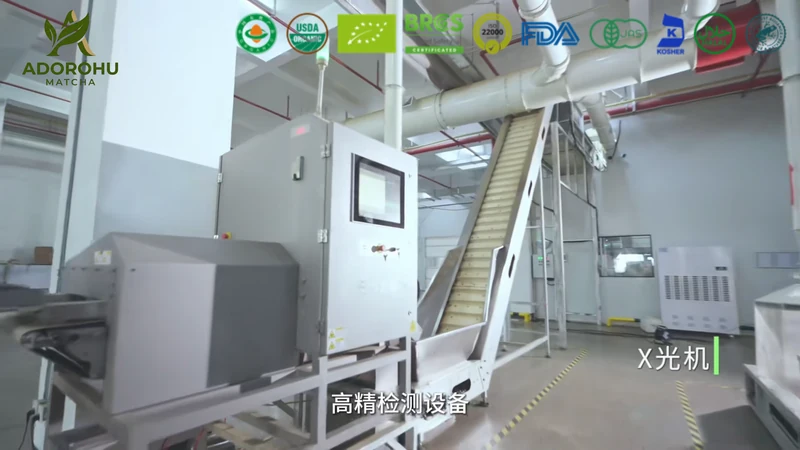
Select metal detection or X-ray from the target material, product effect, package, line speed and reject design. The literature review shows technologies have different material and size capabilities. There is no universal detector or sensitivity setting for matcha. Validate with representative product, pack and challenge pieces at relevant positions.
Metal detection fits detectable metals where product effect, aperture, package, speed, and environment allow stable performance. X-ray detects density differences and may find some metal, glass, stone, or bone under suitable conditions, but it does not detect every material or position.
Select equipment from the target contaminant and actual presentation. Foil packaging, dense product, overlapping packs, contaminant orientation, and location can alter capability. Avoid promising a universal sensitivity: an unsupported threshold creates false release confidence and disputes when the real line cannot reproduce it.
Record the validated product family and pack configuration. Extending a setup to a new density, aperture, or package requires technical review because the product effect and detection geometry may change.
| Technology | Useful target | Important limitation |
|---|---|---|
| Sieve or screen | Oversized material in flowing powder | Cannot identify all material below aperture |
| Magnet | Susceptible ferrous material | Does not capture all metals |
| Metal detector | Validated metal targets | Product, aperture, package, and speed affect response |
| X-ray | Suitable density contrast | Low-density material or unfavorable position may escape detection |
Key Takeaway: Select metal detection or X-ray from the target material, product effect, package, line speed and reject design.
How should detector challenge checks be designed?
Challenge the full operating system with traceable test pieces appropriate to the validated setup. Confirm detection, alarm or signal, reject action, reject-bin security, line stop where used, and failed-check response. The FSIS foreign-material directive describes verifying detection equipment with seeded samples of a specified size and maintaining calibrated limits. That directive governs meat and poultry establishments, so it is supporting process evidence rather than direct matcha regulation; the matcha line needs its own validated conditions.
Place checks at times that bound production exposure, including startup, changeover, end of run, or defined intervals based on the plan. If a check fails, hold product since the last acceptable result until investigation supports disposition. Passing a retest after adjustment does not automatically release the earlier interval.
Test pieces should be controlled, identified, and recovered so the challenge itself cannot contaminate product. Record who performed the check and whether every challenged pack reached the intended reject location.
Key Takeaway: Challenge checks should verify the operating system, including detection, signal, reject, confirmation and failed-check response.
How should hard or sharp objects be assessed?
Assess composition, size, shape, hardness, intended consumer, intended use, and downstream processing. FDA’s hard-or-sharp-object compliance policy discusses 7–25 mm objects for certain ready-to-eat or minimally prepared foods. It also recognizes context and special-risk groups.
The 7–25 mm range is not a universal pass limit, procurement specification, or detector threshold. Objects below 7 mm may still matter, and a processor may alter or remove an object downstream. Escalate findings through qualified hazard assessment rather than releasing product because one dimension falls outside a quoted range.
Measure and describe the actual object without forcing it into a convenient category. Photographs with scale, preserved samples, and material examination support a better source investigation and customer response.
| Assessment input | Question | Why it changes the decision |
|---|---|---|
| Material and shape | Can it cut, puncture, or damage teeth? | Defines injury mechanism |
| Size and orientation | What dimensions matter in use? | Avoids one-number judgment |
| Consumer | Are special-risk groups exposed? | Smaller objects may remain significant |
| Downstream use | Is there validated removal or further processing? | Changes, but does not erase, exposure |
Key Takeaway: Assess material, size, shape, intended use, consumer and downstream processing rather than using one universal threshold.
What happens after a foreign-material finding?
Stop and segregate affected material, preserve the object and package, bound exposure and investigate source before disposition. Record lot, time, line, location, photographs, dimensions, composition, equipment state and related findings. Do not discard the object or restart without an authorized assessment. Extend the hold when last-good evidence is uncertain.
Stop or control the process, segregate affected material, preserve the object, and bound exposure by time, lot, equipment, and distribution. Photograph and identify the finding without destroying evidence. Examine upstream sources and related lots before deciding that the event is isolated.
Disposition may include rejection, controlled rework, further inspection, or other authorized action supported by the hazard and process assessment. Link the investigation to matcha recall planning if distributed product may be affected. Do not use a negative microbiological result as evidence that physical contamination is controlled.
Rework needs its own assessed route and acceptance evidence. Passing affected product through the same unchanged control may repeat the failure or leave contaminants that the device cannot detect.
Key Takeaway: Stop and segregate affected material, preserve the object and package, bound exposure and investigate source before disposition.
How should trends drive CAPA and supplier action?
Trend incidents by material, source, line, supplier, lot, location and recurrence, then verify corrective action effectiveness. Separate isolated ingress from systematic wear or supplier recurrence. Request supplied-lot evidence when needed. Close CAPA only after implementation and follow-up evidence.
Trend findings by material type, suspected source, equipment, supplier, product, line, shift, and time. Normalize by production or receipts where possible so higher volume does not automatically look worse. Preserve uncertain classifications rather than assigning a convenient source.
Repeated fragments, rising counts, or similar customer complaints should open investigation and corrective action. Verify effectiveness with source removal or sustained evidence, not retraining alone. Buyers can compare the program with published matcha particle-size specification guidance while keeping particle-size performance separate from hazardous foreign material.
Close corrective action only after the changed control has operated under representative conditions. One quiet shift may be insufficient where the suspected wear mechanism develops over longer production runs.
For records tied to a specific lot or package, state the finding, product code, lot, and intended use when making the request.
Key Takeaway: Trend incidents by material, source, line, supplier, lot, location and recurrence, then verify corrective action effectiveness.
FAQ
- What is foreign material in food?
- It is unwanted physical material from ingredients, equipment, people, packaging or the environment.
- Can one detector find every foreign material?
- No. Capability depends on material, size, product, package, position and validated settings.
- Is 7 mm a universal FDA limit?
- No. FDA policy has a defined scope and smaller objects can matter in some circumstances.
- How often should detectors be challenged?
- Set frequency from the validated control, risk, process and applicable requirements.
- What should happen after a finding?
- Segregate product, preserve evidence, bound exposure, investigate and document disposition.
- Does microbiological testing cover foreign material?
- No. Microbiological and physical-contaminant controls answer different hazards.
Conclusion
The next decision is whether the supplier has matched credible physical sources to prevention, suitable detection, challenge verification, and controlled incident disposition. Reject universal threshold claims that are not reproduced on the actual product and line. Request lot-specific records through AdoroHu Matcha when a buyer needs to close a defined review.