Matcha solubility tests work for beverage buyers when they separate wetting, dispersion, settling, and redispersion in the intended formula. Whole-leaf matcha forms a suspension; it does not behave like a fully soluble instant tea extract. A clear cup immediately after mixing can still form sediment later.
The wrong test creates expensive surprises during scale-up: clumps, package separation, color gradients, gritty mouthfeel, or sediment that will not redisperse. Build the matcha solubility test around powder from an application-relevant matcha supply, then lock the formula, process, package, observation schedule, and acceptance limits.
Matcha solubility is better treated as a set of physical-performance tests than as one percentage. Measure how the powder wets and disperses, how particles settle, what the sediment becomes, and whether the packaged drink redisperses as intended. Approve the powder in the real beverage matrix and process, not only in a fresh glass of water.
In short:
Key points:
- Distinguish molecular dissolution from particle dispersion, suspension stability, sedimentation, and redispersion.
- Lock the matcha lot, dose, matrix, ingredient order, temperature, pH, shear history, package, and storage conditions.
- Set application-specific limits; research conditions and particle sizes are evidence examples, not universal commercial specifications.
Does Matcha Solubility Mean the Powder Fully Dissolves?
Matcha solubility does not mean whole-leaf powder fully dissolves. Water-soluble compounds can move into the liquid, while insoluble leaf particles remain dispersed and may later settle. A soluble tea extract is a different ingredient category because most insoluble material has been removed before drying.
This distinction changes the purchase specification. If the buyer writes only “good solubility,” one supplier may report extractable solids while another reports visual clumps after mixing. Both could claim compliance while measuring different endpoints.
| Term | Practical meaning | Typical failure |
|---|---|---|
| Dissolution | Molecules enter solution | Insoluble material remains |
| Wetting | Liquid displaces air around powder | Floating islands and dry cores |
| Dispersion | Particles distribute through the liquid | Clumps and concentration gradients |
| Sedimentation | Suspended particles move downward | Visible layer or uneven serving |
| Redispersion | Settled particles return after defined mixing | Compact or caked sediment |
Replace one vague matcha solubility claim with separate test endpoints.
Key Takeaway: Whole-leaf matcha is a suspension system, so dissolution, dispersion, settling, and redispersion need separate decisions.
Which Matcha Solubility Question Should a Buyer Ask First?
The first matcha solubility question should identify the customer-visible failure the test must prevent. A made-to-order latte may only need fast, repeatable incorporation at the bar. A bottled RTD may need acceptable uniformity, sediment appearance, redispersion, mouthfeel, and color through its validated shelf life.
Write the use case before the method:
- beverage matrix and serving format;
- intended process and equipment;
- package, storage, and transport conditions;
- whether the consumer will shake the product;
- visible, sensory, dosing, and operational limits.
This boundary keeps a bench test honest. A powder can pass a short incorporation test and still fail a package-uniformity requirement. Conversely, some visible loose sediment may be acceptable when the label instructs shaking and the product redisperses cleanly.
Key Takeaway: Define the unacceptable product behavior first, then select the measurements that reveal it.
How Does Particle-Size Distribution Affect Matcha Settling?
Particle-size distribution can affect matcha settling because smaller particles often settle more slowly under otherwise comparable conditions. A 2003 original matcha study compared a classified fine fraction with its processing-matcha source.
For those samples, median diameters were 3.2 micrometres and 11.5 micrometres, while D90 values were 6.9 and 39.4 micrometres. The researchers whisked 1% and 2% weight/volume suspensions in distilled water near 25°C and visually followed sediment from 15 to 240 minutes. At 240 minutes in the 1% test, the reported sediment lines were 0.9 and 7.0 mL per 100 mL.
Those values describe the study samples and method. They are not universal grade limits or proof of RTD shelf stability. Ask for the distribution and coarse tail with the measurement method; an average or mesh claim can hide particles that dominate visible settling.
Key Takeaway: Particle distribution can explain settling, but a supplier number must be verified in the finished beverage rather than copied into a universal limit.
Why Can a Matcha Solubility Test in Water Fail in Milk?
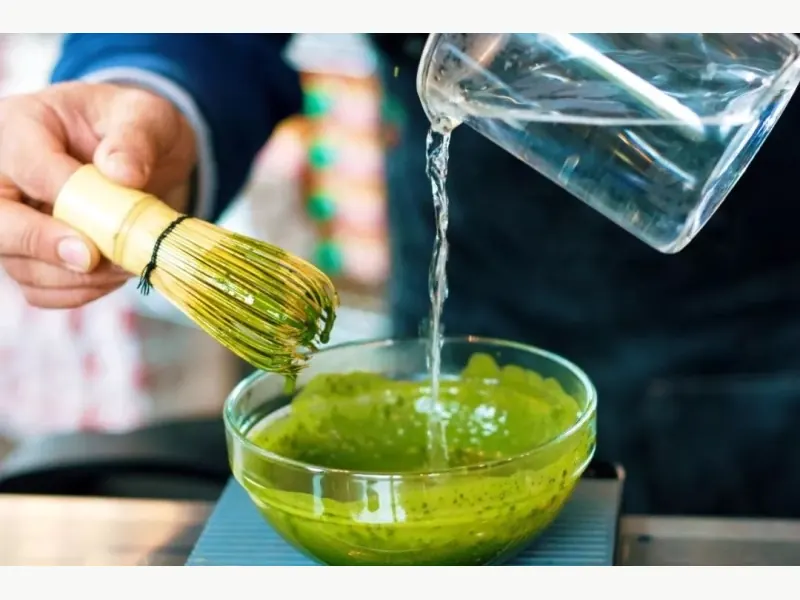
A matcha solubility test in water can fail in milk because the matrix changes wetting, viscosity, particle interactions, and suspension behavior. Protein, fat, minerals, sugar, pH, gums, heat, and ingredient order can all change how the same powder performs.
A 2016 study of matcha milk tea treated the system as a rheology and suspension problem and evaluated a particular stabilizer combination. Its reported levels and viscosity applied to that experimental formula. They should not be copied into dairy, plant-based, acidic, or clean-label products without new formulation and regulatory review.
Use simple water as an early screen, then move quickly into the actual base. The beverage-brand sourcing guide explains the broader formulation context. Rejecting a powder from water alone can discard a workable candidate; approving it from water alone can hide an expensive matrix failure.
Key Takeaway: Water is a screening medium, while the intended milk, RTD, syrup, or plant base is the approval medium.
What Inputs Must a Matcha Solubility Test Lock?
A matcha solubility test must lock every input that could change incorporation or settling. At minimum, record the powder lot and dose, finished formula, ingredient order, temperature, pH, solids, protein, fat, minerals, and any stabilizer.
Process details matter just as much:
- mixer type, vessel geometry, speed, time, and powder-addition rate;
- pre-slurry or direct-addition method;
- heat, hold, homogenization, cooling, and filling sequence;
- package, fill volume, headspace, closure, and storage orientation;
- handling or transport simulation and intended shake instruction.
AdoroHu Matcha uses 20 stone mills, 56 ball mills, 8 continuous ball mills, and an ultrasonic screening system. For the sampled lot, ask which milling and screening route applied and preserve that route in the approval record. Those assets do not imply a universal particle-size distribution or finished-RTD result, but the record helps reproduce a chosen sample and investigate later change.
Do not substitute a supplier's powder-production equipment for the buyer's liquid-process validation. Milling, screening, or a dry homogenizer may improve raw-material consistency, but it does not prove performance in a commercial RTD mixer, heat process, or package.
Key Takeaway: Lock the full formula and process history so a changed result can be traced to a changed input.
What Should Matcha Solubility Tests Measure Separately?
Matcha solubility tests should measure incorporation, dispersion, separation, sediment character, redispersion, and sensory performance as separate outputs. One visual score immediately after mixing hides too much.
| Output | Example record | Buyer consequence |
|---|---|---|
| Wetting/incorporation | time, floating powder, dry cores | labor and batch time |
| Dispersion | screen residue, concentration at vessel heights | dose uniformity |
| Separation | first visible change at defined observations | shelf appearance |
| Sediment | amount, loose/compact/caked character | package rejection risk |
| Redispersion | defined inversions or shake cycle | consumer usability |
| Product quality | viscosity, color, mouthfeel, flavor | brand consistency |
Set observation points from the product's real use, shelf-life plan, and decision risk. There is no responsible universal settling time for every matcha drink. Record exact times and conditions so later lots can be compared against the same method.
Key Takeaway: Separate the outputs and define their observation schedule; a single “pass” hides the failure mode.
How Should a Bench Matcha Solubility Test Be Run?
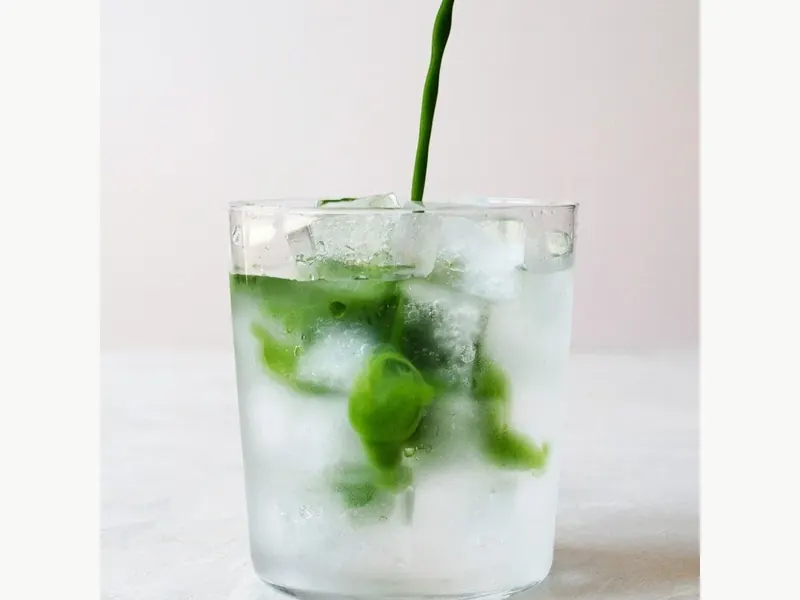
A bench matcha solubility test should use a controlled procedure that can be repeated before scale-up. Prepare enough replicates to expose method variation, include the approved reference, and randomize or blind samples when sensory judgment is involved.
A practical sequence is:
- verify ingredient identities and condition samples to the stated test temperature;
- prepare the complete matrix in a fixed ingredient order;
- add the matcha through the defined route and record incorporation time;
- sample from defined vessel positions for initial uniformity;
- fill the intended package and apply the planned process;
- inspect at predefined times without disturbing the package;
- apply a defined redispersion action and score the result;
- record color, mouthfeel, flavor, and any screen residue.
Use the latte-grade selection guide when the target is a cafe or milk beverage. For RTD development, extend the test into the validated thermal process, package, storage, and shelf-life program.
Key Takeaway: A bench test is useful when its formula, process, package, timing, and scoring can be repeated by another operator.
How Should Matcha Solubility Scale From Bench to Production?
Matcha solubility should scale through staged confirmation because shear and flow do not transfer directly from a beaker to a production vessel. Mixer diameter, tip speed, turnover, dead zones, powder-feed rate, batch size, heat load, and hold time can change both dispersion and sensory quality.
Scale by process evidence rather than matching a single rpm value. Hold the formula and critical material attributes steady, then compare incorporation, vessel uniformity, sediment, redispersion, color, and flavor at pilot and production scale.
Avoid solving every problem with more shear. Higher energy may reduce visible clumps while adding heat, foam, oxidation, or equipment constraints. Choose the lowest process intensity that meets the finished-product acceptance criteria consistently.
Key Takeaway: Scale the physical result and product quality, not an rpm number taken from different equipment.
How Should a Buyer Approve a Matcha Solubility Specification?
A buyer should approve a matcha solubility specification only after the candidate powder passes the intended formula, process, package, and decision rules. The file should distinguish alert limits from rejection limits and state what requires retest, investigation, reformulation, or supplier action.
Connect the application record to the matcha clumping guide for immediate preparation problems, but keep that consumer-facing issue separate from long-term sedimentation. A clump-free cup at minute zero is not evidence of package stability.
A strong approval record includes:
- matcha lot, reference lot, formula version, and package identity;
- raw-material particle data with method, when relevant;
- controlled process and observation schedule;
- separate acceptance criteria for incorporation, uniformity, sediment, redispersion, and sensory quality;
- deviation, retest, hold, and change-control rules;
- pilot and production confirmation before routine purchasing.
Key Takeaway: Approve the complete application-performance file, not a supplier claim that the powder is “soluble.”
FAQ
Does matcha fully dissolve in water?
- No. Whole-leaf matcha releases soluble compounds while insoluble particles remain suspended and may later settle.
Is finer matcha always better for every beverage?
- No. Particle-size distribution can affect settling and mouthfeel, but the formula, process, package, sensory target, and coarse-particle tail also determine performance.
How long should a matcha sedimentation test run?
- Use observation times tied to the product's preparation, storage, shelf-life, transport, and serving conditions; there is no universal duration for every beverage.
Can a water test approve matcha for an RTD latte?
- No. Water can screen candidates, but approval should use the intended dairy or plant-based matrix, process, package, and storage conditions.
Does visible sediment automatically mean poor matcha quality?
- No. Sediment can reflect particle distribution, formula, process, storage, or the acceptance rule; evaluate its amount, character, redispersion, and effect on the product.
Conclusion
Matcha solubility testing becomes useful when it stops pretending that a whole-leaf suspension is a soluble extract. Define the failure, lock the matrix and process, measure separate endpoints, and confirm the result at scale. Contact AdoroHu Matcha to discuss grade samples and technical information for your beverage application.